Process guide
CNC plasma cutting: process and cut quality
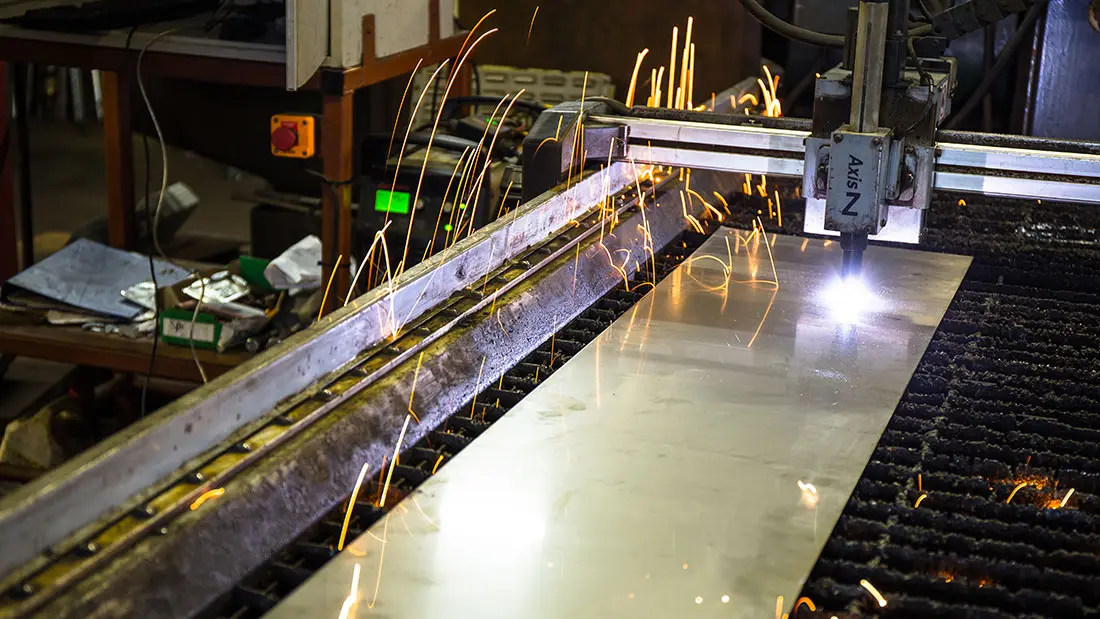
What to expect from plasma-cut edges, holes, fine detail and centre marks for later drilling.
Current machine facts included Open item
 Basket (0)
Your basket is empty. Choose something from the shop to get started.
Total inc VAT£0.00
Demo prices · delivery quoted separatelyProjects & updates
Case studies, process guidance and recent work from the workshop and customer sites, published after the details and permissions have been checked.
Process guide
What to expect from plasma-cut edges, holes, fine detail and centre marks for later drilling.
Current machine facts included Open itemLocal fabrication
A 3 mm checker-plate lid made to fit an existing cast-iron frame, stiffened with 50 × 5 mm flat-bar bracing and galvanised after fabrication.
Final weight and photographs to confirm Open itemLocal fabrication
The customer required a nominal 850 mm square replacement cover for an existing cast-iron frame. The finished arrangement used an approximately 840 mm lid, 830 mm support angle and 5 mm nominal rim.
Three-millimetre checker plate was selected to keep the weight down, with a corner-to-corner X-brace made from 50 × 5 mm flat bar for stiffness. Short drop handles allowed normal opening without tools, while standard drain-key holes were provided when more lifting force was needed. Galvanising was arranged after fabrication.
The recorded finished weight is approximately 31 kg and must be confirmed before publication.
Archived process article
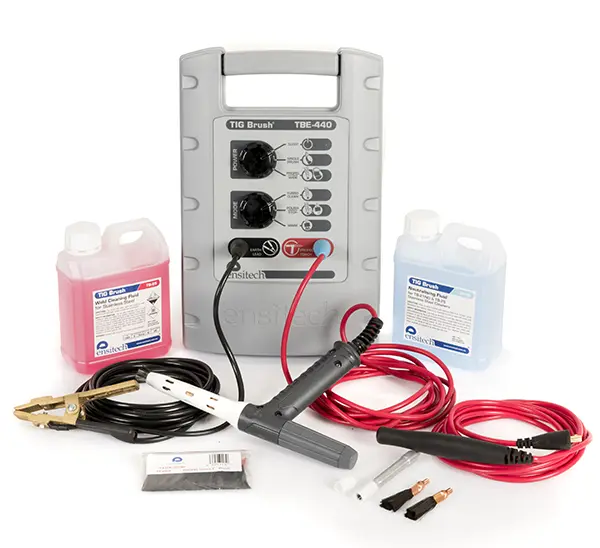
An older Peter Mitchell & Son article explains the move from abrasive finishing or hazardous pickling paste toward electrochemical weld cleaning using phosphoric-acid solution. It also describes applying a permanent dark oxide mark through a stencil.
The archived article will be checked against the current equipment, consumables and safety information before it is republished.